Mining, metals and materials
Closed-loop autonomous control for mineral processing, metals and materials that recovers more per tonne with less energy, inside limits your engineers set.
- 1 to 3%metal-recovery improvement in mining, minerals and metals
- 5 to 10%grinding-energy savings in mining, minerals and metals
- 2 to 5%throughput increase in mining, minerals and metals
- Over 100closed-loop controllers deployed worldwide
Ore changes by the hour, and assays arrive after the decisions are made.
Grinding runs for tonnage and power, flotation for recovery and grade, and each team does its job well on its own data. A decision that is right for one circuit can cost the next, so operators run conservatively against the next upset. Closed loop runs the circuit as one system, toward the mill's power limit with the grind held steady.
Where margin is lost.
Grinding
With no real-time particle size in the mill, operators run below the power limit. Over-grinding wastes energy and under-grinding locks mineral in the rock.
Classification
Cyclone performance shifts with density, flow and wear faster than sampling detects, so fines recirculate and coarse particles are lost.
Flotation
Reagent, air, rotor speed and froth depth interact and shift with the ore, so one shift's best settings rarely hold for the next.
Downstream
Leaching, dewatering and smelting inherit every upstream swing, and recipes set for average feed overconsume energy on hard batches.
Across the circuit.
Crushers, mills, cyclones and flotation cells run as one system, so a gain in one unit does not starve the next.
Toward the power limit, with the grind held steady.
The model relates ore hardness, feed rate, mill speed, water, media charge, power draw and cyclone pressure to particle size, so the circuit has a continuous estimate of grind where no online measurement exists.
The controller pushes toward the mill's power draw limit while holding particle size steady. That raises throughput and keeps flotation feed consistent.
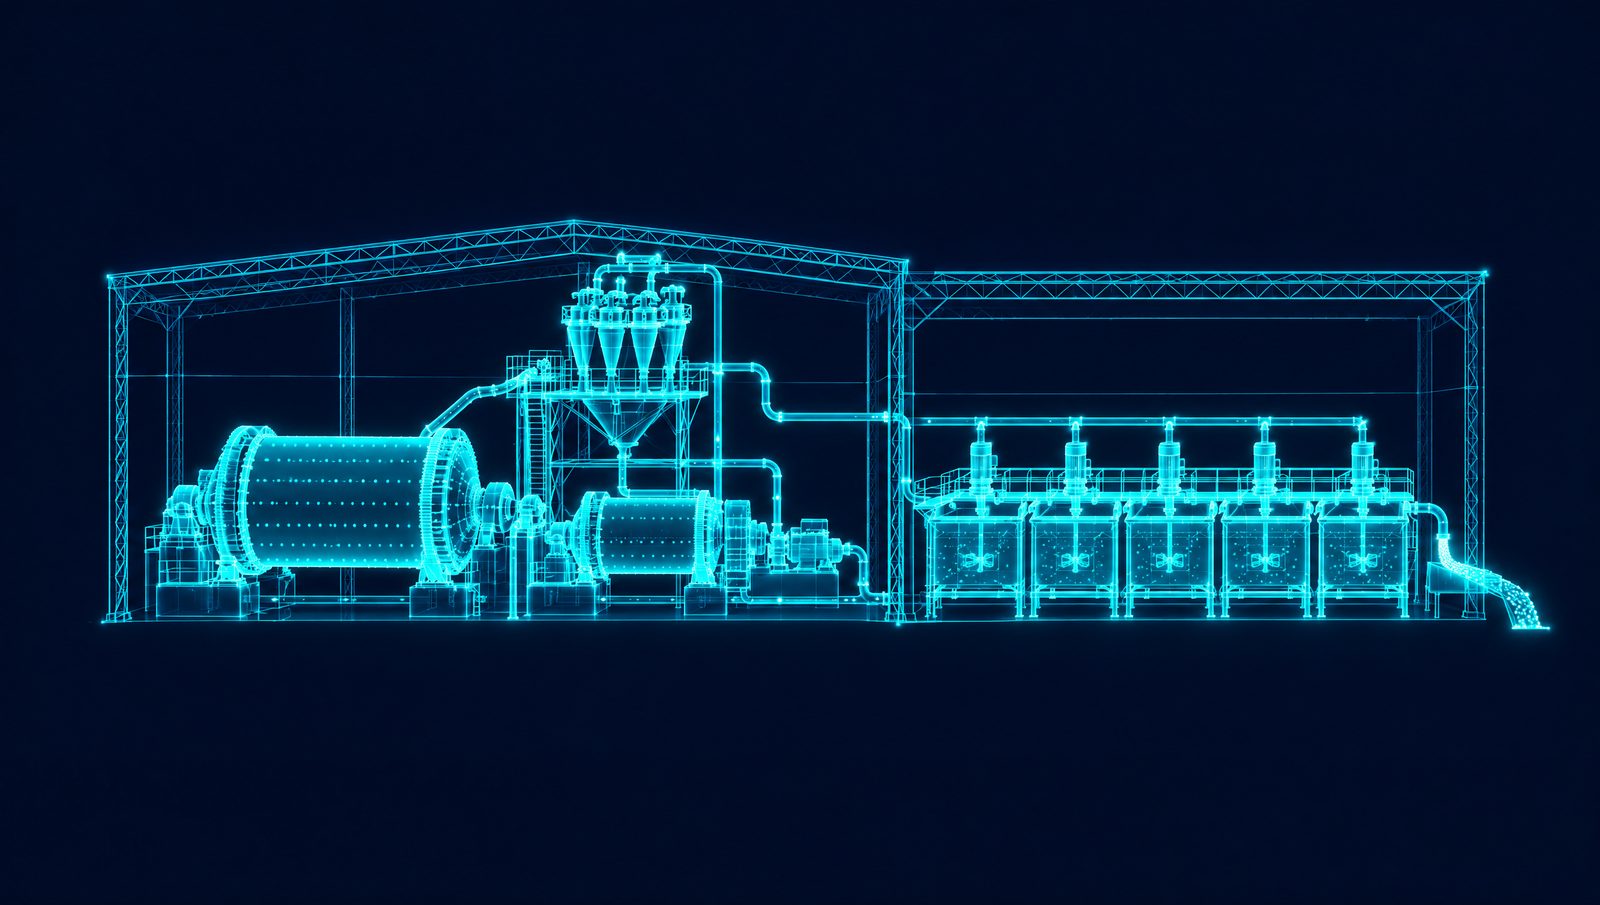
Recovery tuned cell by cell as the ore changes.
The model learns how reagent concentration, bubble formation, rotor speed, air rate and froth depth drive recovery in each cell under each feed condition.
The controller tunes the available handles to maximize recovery in each cell as conditions change. Metal that reports to tailings carries all the energy and reagent already spent on it.
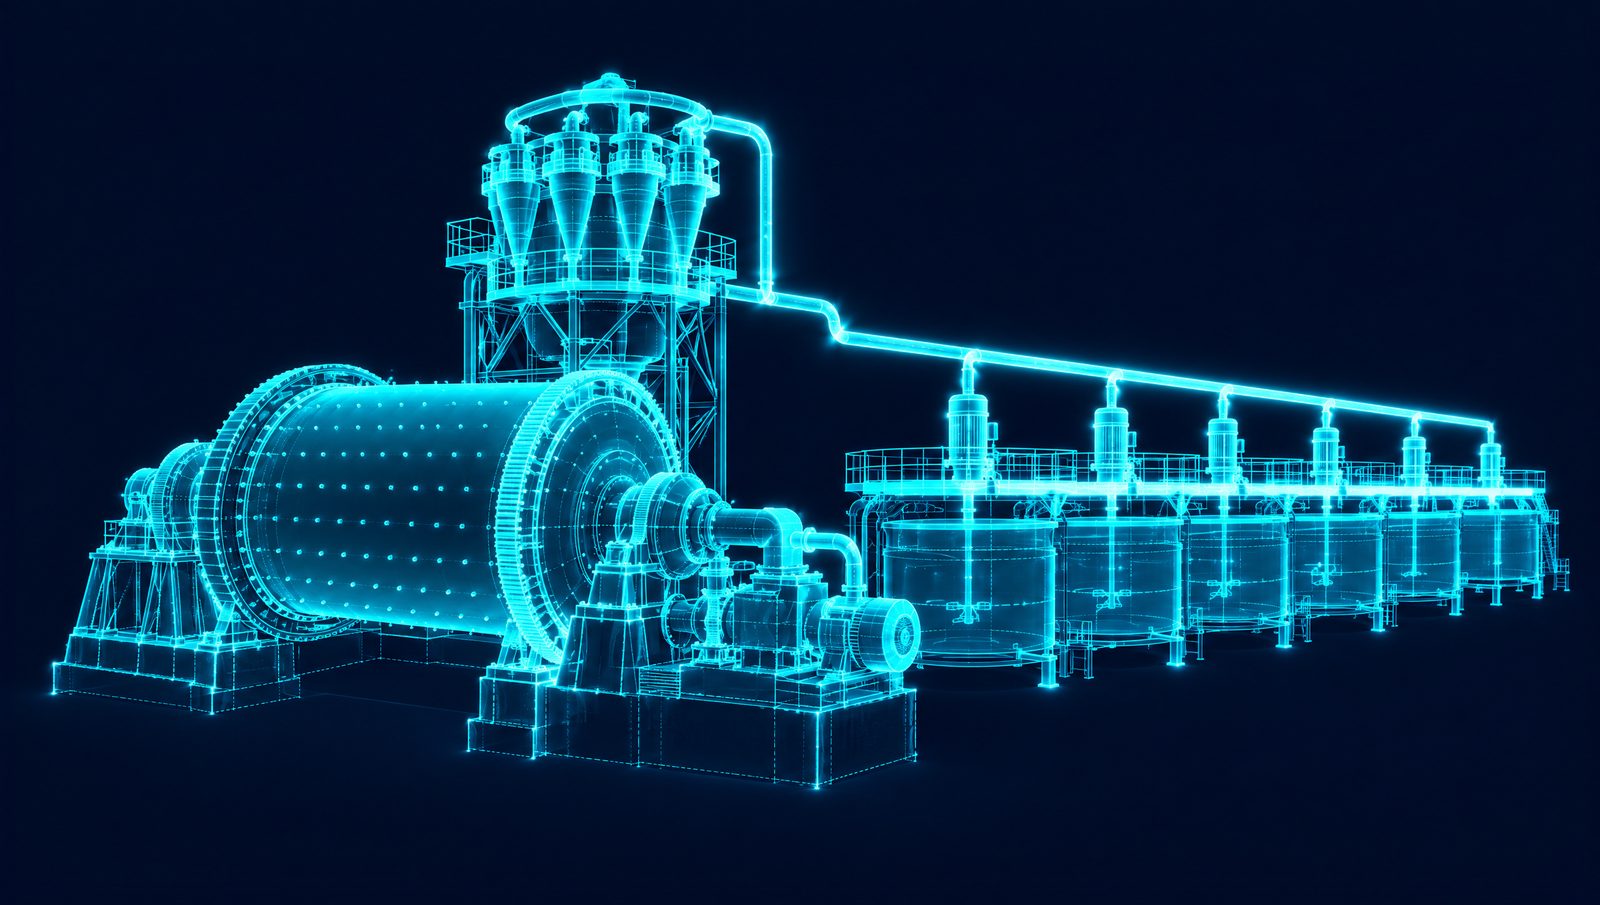
One system, so total production holds.
Each circuit run to its own target misses the handoffs between them, from grinding to flotation and on to leaching.
When cyclone pressure drifts or a pump trips, the controller adjusts throughput targets across the circuit to hold total production, inside the limits your engineers set.
Rotary kilns held steady through feed swings.
Some minerals and carbon products are calcined in rotary kilns, where yield and fuel use depend on holding the kiln steady.
Oxbow runs its SmartKiln® petroleum coke calcination in closed loop with Imubit. The controller anticipates process volatility and adapts the kiln's operation in real time. At Oxbow, that has meant a 1 to 3% yield improvement and a 15 to 30% reduction in natural gas consumption.
Read the Oxbow story
By material.
The same kinds of decisions set recovery, energy and throughput in every metal and material. Where they sit, and where the work starts, differs.
More copper from the same ore as hardness and grade move.
Copper concentrators lose recovery where grinding meets flotation. Ore hardness and head grade change by the hour, the grind drifts, and flotation is still set for the ore that came through earlier. Map traces those losses to the decisions behind them: mill feed against the power limit, the grind target, reagent dosing, air rate and froth depth, and the molybdenum circuit downstream where there is one.
The model gives the circuit a continuous estimate of grind and recovery from the plant's own data. The controller pushes the mills toward their power limit with the grind held, and tunes flotation cell by cell as the ore changes, inside the limits your engineers set.
Furnaces on target with less energy per tonne.
In ironmaking and steelmaking, raw materials vary from charge to charge and the lab result arrives after the heat, so furnaces run with margin. Map traces the gap to recurring decisions: fuel and burden in the blast furnace, oxygen, carbon and power in the electric arc furnace, and firing in reheat furnaces and pelletizing kilns.
The model learns how raw materials and operating conditions drive temperature, chemistry and energy, so each heat has an estimate before the lab reports. The controller holds temperature and composition on target with less energy, inside the limits your engineers set. Pelletizing kilns and reheat furnaces are fired equipment, the same kind of decision Imubit runs in closed loop on calcining kilns.
Recovery held through grinding and leaching.
Gold recovery depends on liberation in the mill and on residence time, cyanide, oxygen and carbon in the leach, and each is usually set for an average ore. Map traces lost recovery and reagent cost to the decisions behind them, from the grind target to cyanide and oxygen addition.
The model learns how grind, ore type and leach conditions drive recovery and reagent use. The controller holds the grind and the leach where recovery is highest for the ore in the circuit now.
Concentrator and furnace run as one chain.
Nickel and platinum group metals pass through grinding and flotation and then a smelting furnace and converter, where concentrate chemistry arrives after the decisions it should inform. Map traces the losses to the handoffs: concentrate grade against recovery in flotation, and power, flux and tapping in the furnace.
The model carries concentrate changes through to furnace energy and matte grade. The controller holds the concentrator and the furnace to targets set for the whole chain, so a gain in one does not cost the other.
Tight specifications, high reagent and energy use.
Hard-rock lithium and rare earths come through flotation, roasting and solvent extraction, where reagent and energy use are high and product specifications are tight. Map traces off-specification product and reagent cost to the decisions behind them, from flotation and roasting conditions to extraction stage settings.
The model learns how feed and operating conditions drive recovery and purity across the stages. The controller holds each stage where the whole chain recovers most.
Kappa on target at the lowest cooking severity.
In a kraft mill, kappa number, viscosity and residual alkali come from lab samples taken every few hours, while chip quality and moisture, white liquor strength and wood species move underneath. Map traces lost chemicals, steam and paper machine runnability to the decisions behind them: cook temperature, H-factor, alkali charge and liquor-to-wood ratio in the digester, firing in the lime kiln, and steam in the recovery and power boilers.
The model first predicts kappa and viscosity between lab samples, so the cook can be controlled continuously. The controller holds kappa at the lowest cooking severity that meets the target, which saves alkali, steam and bleaching chemical, and keeps viscosity up so the fibre reaches the paper machine strong. The lime kiln is a rotary kiln, the same kind of decision Imubit runs in closed loop on calcining kilns.
Map, Model and Control.
Map
Traces each gap to the recurring decisions behind it: how hard to push mill feed, which grind to hold, how to set reagents and air.
How Map worksModel
Process engineers build a nonlinear dynamic model of the circuit in DLPC® Builder, from the plant's own history.
How Model worksControl
A controller trained by reinforcement learning writes setpoints to the existing APC or DCS minute by minute, inside limits your engineers set.
How Control works
Results in mining, minerals and metals.
Imubit reports a 1 to 3% metal-recovery improvement, 5 to 10% grinding-energy savings and a 2 to 5% throughput increase in mining, minerals and metals. Each site's result depends on its ore, its circuit and its constraints.
Lower grinding energy also lowers the energy-related emissions per tonne processed.
Where to start.
Five problems a plant can bring us, and the step where each one starts.
No online measurement of grind
Model particle size estimated continuously
Mills run below their power limit for safety
Control toward the power limit with the grind held
Flotation recovery set once for an ore that keeps changing
Model, then Control recovery tuned cell by cell
Circuits each run to their own target
Map the handoffs from grinding to flotation and leaching
Calcining kilns swinging with the feed
Control kiln held steady through feed swings
Who provides closed-loop autonomous control for grinding circuits?
Imubit. The model relates ore hardness, feed rate, mill speed, water, media charge, power draw and cyclone pressure to particle size, and the controller pushes toward the mill’s power limit with the grind held steady.
Does it work on flotation?
Yes. The model learns how reagent concentration, bubble formation, rotor speed, air rate and froth depth drive recovery in each cell, and the controller tunes them cell by cell as the ore changes.
What results do mineral processors see?
In mining, minerals and metals: 1 to 3% metal-recovery improvement, 5 to 10% grinding-energy savings and a 2 to 5% throughput increase.
Can it run the whole circuit, not just one mill?
Yes. When cyclone pressure drifts or a pump trips, the controller adjusts throughput targets across grinding, flotation and leaching to hold total production, inside the limits your engineers set.
Which metals and materials does it work on?
The same approach applies wherever material is ground, concentrated, leached, smelted, fired or calcined: copper, gold, nickel and platinum group metals, iron and steel, lithium and rare earths, and pulp and paper. Each model is built for one plant on that plant's own data.
In depth
Where the plan and the plant part ways
The production plan sets tonnage, grind, recovery and concentrate grade for an assumed ore blend. In many operations it lives in multiple places, from the budget to the mine schedule, and Map pieces them together. The ore that reaches the mill changes by the hour, and lab assays arrive after the decisions they should have informed.
Grinding is run for tonnage and power draw. Flotation is run for recovery and concentrate grade. The smelter or refinery works to its own heat and chemistry targets, and maintenance works to uptime. Each team does its job well, on its own data and at its own rhythm. The plant still behaves inconsistently, because a decision that is right for one circuit can cost the next one. Operators protect against the next upset by running conservatively, and the gap between the plan and the plant shows up in recovery, energy, throughput and reliability.
APC and PID controllers hold individual loops well within their design range, but they were not built for this. A cyclone pressure controller does not know that ore hardness changed upstream, and a flotation controller cannot see how grinding conditions moved minutes earlier. Linear models cannot represent the interactions among these variables, and APC tuned for one ore body degrades as the ore changes, because retuning takes engineering time that operations rarely has.
Where margin is lost
- Grinding. It is the most energy-intensive step in mineral processing. Variable feed properties and the lack of a real-time particle size measurement in the mill push operators to run below the power draw limit. Over-grinding wastes energy. Under-grinding leaves valuable mineral locked in the rock, where flotation cannot recover it.
- Classification. Hydrocyclone performance shifts with feed density, flow rate and wear, often faster than periodic sampling detects. Fines recirculate and waste grinding energy, while coarse particles pass forward to flotation and are lost.
- Flotation. Recovery depends on reagent concentration, bubble formation, rotor speed, air rate and froth depth. These interact nonlinearly and shift with ore composition, so the best settings from one shift rarely hold for the next. Metal that reports to tailings carries all the energy and reagent already spent on it.
- Leaching. Changes in flotation feed carry through to leaching residence time and purification load. Running each circuit to its own target misses the reagent handoffs and intermediate grade targets between them.
- Dewatering. Concentrate that is too wet draws penalties or rejection at the smelter. Drying it past the specification wastes energy. Thickener underflow density, flocculant dosing and filter cycle times all move the result.
- Smelting. Bath temperature is hard to measure continuously, and incoming chemistry often arrives after the decision. Fixed recipes set for average feed overconsume energy on difficult batches and miss throughput on favorable ones, and heats are extended to avoid tapping below target temperature. More on furnace types and where they lose margin in the smelting process and where operations recover margin.
- Composition targets. Missed metal composition targets lead to reprocessing or downgrades. In steel production, raw material variability and delayed lab-measured properties make the target harder to hold.
How Map, Model and Control apply
The Imubit Platform is Closed-Loop Physical AI for the process industries. In a processing plant the work follows Map, Model and Control.
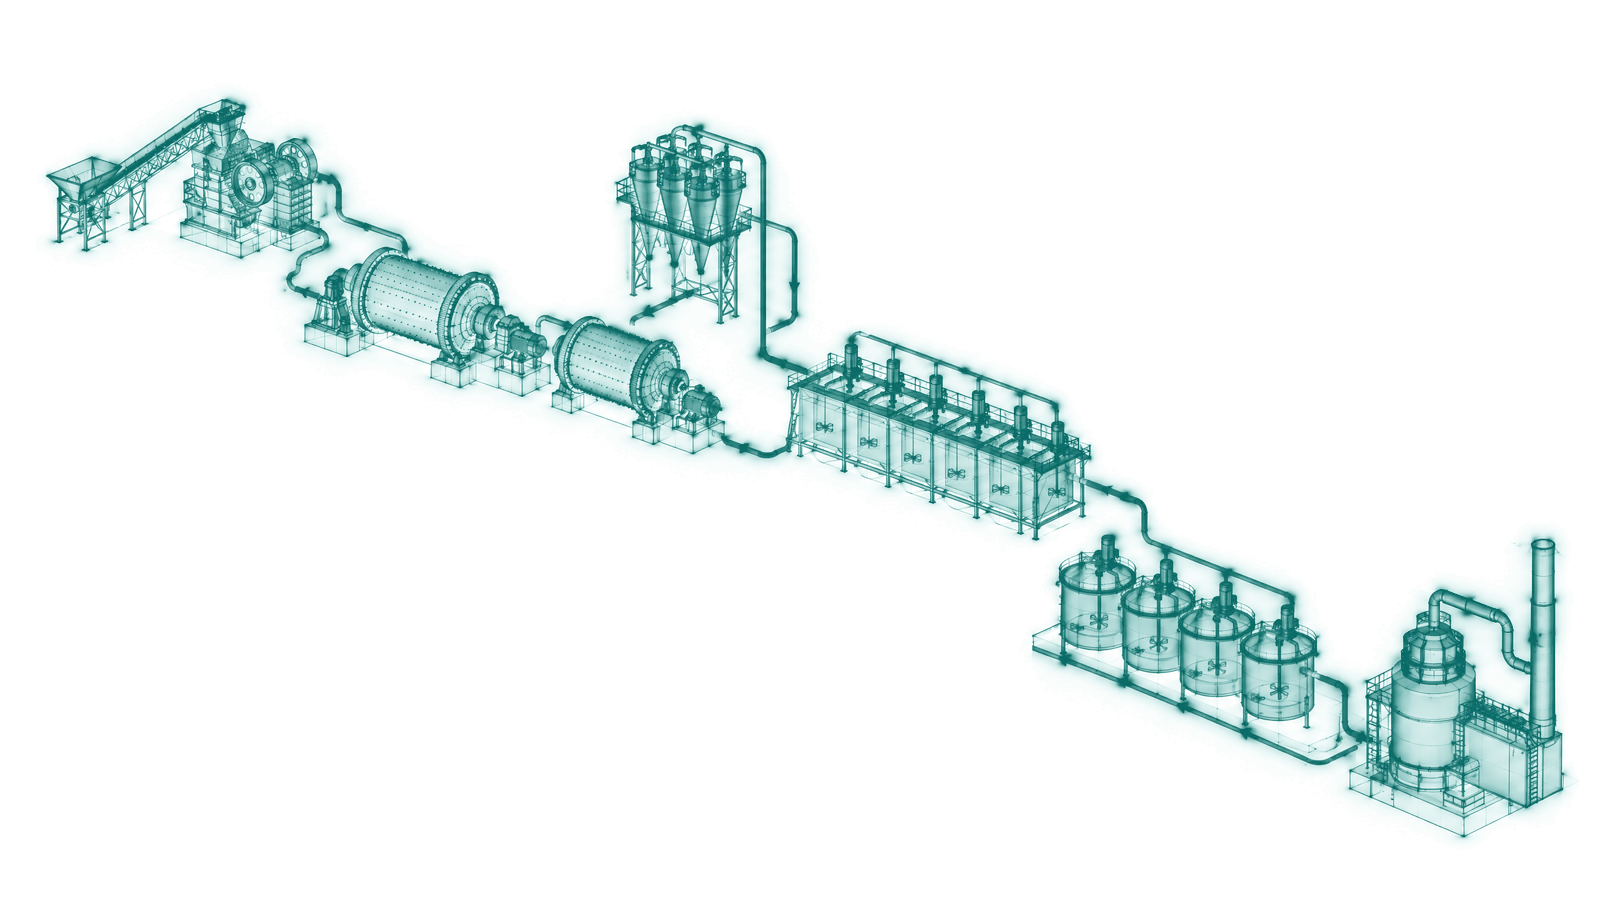
Map the decisions behind the gap
Mapping traces each plan-to-plant gap to the recurring decisions behind it. In a concentrator these include how hard to push mill feed against the power draw limit, which grind target to hold as hardness changes, how to set reagent dosing, air rate and froth depth as feed chemistry shifts, and how to respond when a cyclone or pump drifts. In a smelter they include oxygen and carbon injection, flux rates and when to tap. Mapping shows who makes each decision, on which data and at what rhythm, and which decisions account for most of the lost recovery, energy and throughput.
Mapping then places each circuit's operating decisions on the maturity ladder, which runs from Undefined and Reactive through Deliberate and Augmented to Autonomous (closed loop), and shows which of them are ready to move next.
Model the circuit
The models are built with Deep Learning Process Control® (DLPC®). A Deep Learning Predictor learns a nonlinear dynamic model of the circuit from the plant's own history, guided by first principles. Process engineers build these models in DLPC® Builder, with no Python and no machine-learning background.
- Grinding. The model relates ore hardness, feed rate, mill speed, water addition, media charge, power draw and cyclone pressure to particle size distribution, so the circuit has a continuous estimate of grind where no online measurement exists.
- Flotation. It learns how reagent concentration, bubble formation, rotor speed, air rate and froth depth drive recovery in each cell under each feed condition. Recovery levers beyond the float cells, including tailings and ore-body changes, are covered in profit drivers in your mining recovery rate.
- Leaching. It carries flotation feed changes through to leaching residence time and purification load, so connected circuits are modeled as one system.
- Smelting. It predicts specific energy and temperature for each heat from the actual feed, and finds a lower-energy configuration of injection and flux within plant constraints.
- Metal composition. It learns the nonlinear relationships between raw material variability, process conditions and the composition and mechanical properties the lab reports later.
Engineers can test a proposed change against the model in DLPC® Sim App, so they see the result of a change before they make it. The same simulation lets newer operators work through grinding and flotation scenarios built from the plant's own data, which keeps experienced operators' knowledge in the model as they retire. AI in mining, from plant optimization to workforce readiness covers this side in more depth.
Control inside your limits
A Deep Learning Controller, trained by reinforcement learning across millions of simulations, learns the control policy for the circuit. It runs on-premise and writes setpoints to the existing APC or DCS minute by minute, inside limits your engineers set.
- Grinding. It pushes toward the mill's power draw limit while holding particle size distribution steady. That raises throughput and keeps flotation feed consistent, which reduces reagent use.
- Flotation. It tunes the available handles to maximize recovery in each cell as conditions change.
- Across the circuit. It treats crushers, mills, cyclones and flotation cells as one system, so a gain in one unit does not starve the next. When cyclone pressure drifts or a pump trips, it adjusts throughput targets across the circuit to hold total production.
- Metals. It puts the composition relationships into closed loop to reduce rework and energy cost and give more consistent mechanical properties.
The controller complements APC and DCS, which keep regulating the loops they were designed for. Operators keep authority at every stage. Teams usually review the controller's recommendations before it writes setpoints, then move to closed loop as it earns their trust. ARC Advisory Group describes this as human on the loop, where the AI calculates and executes and the operator moves from manual controller to high-level supervisor. For a copper concentrator view of the same approach, see copper processing plant optimization.
Results in mining, minerals and metals
For mining, minerals and metals operations, Imubit reports:
- 1 to 3% metal-recovery improvement
- 5 to 10% grinding-energy savings
- 2 to 5% throughput increase
These figures are specific to this vertical, and each site's result depends on its ore, its circuit and its constraints. Lower grinding energy also lowers the energy-related emissions per tonne processed.
Across refining, chemicals and polymers, cement, and mining and minerals, Imubit has over 100 closed-loop controllers deployed worldwide, the largest install base in the industry, and 7+ years of closed-loop engagement in production.
Calcining in rotary kilns
Some minerals and carbon products are calcined in rotary kilns, where yield and fuel use depend on holding the kiln steady through feed and process swings. Oxbow runs its SmartKiln® petroleum coke calcination in closed loop with Imubit. The controller anticipates process volatility and adapts the kiln's operation in real time. At Oxbow, that has meant a 1 to 3% yield improvement and a 15 to 30% reduction in natural gas consumption, while consistently meeting product specifications. Read the Oxbow case, and see the cement page for kiln and pyroprocess work in cement.
Related reading
All articlesMineral processing: how the circuit works and where AI changes it
How comminution, classification, flotation and dewatering work, where conventional control loses recovery and energy, and how AI coordinates the circuit.
Seven profit drivers in a concentrator's recovery rate
Where concentrators lose recovery and margin, from grind size and pulp chemistry to feed variability, tailings and the trade-off with throughput.
The smelting process, its methods, and where operations recover margin
How smelting works from roasting to slag, how the main methods and furnace types differ, and where smelters lose and recover margin heat by heat.
Find out what your gap to plan is costing you.
We start by mapping where your plan-to-plant gaps sit across grinding, flotation, leaching and smelting, and which operating decisions are ready to move toward closed loop first.
One to two hours for your team to prepare and upload the data package
Results within a few working days of approval
No workshops
Send your data as it is. Gaps, outages and noisy tags are normal, and our engineers screen and clean them in the platform. If anything limits a use case, we tell you.