Closed loop lowers a plant's energy use and emissions.
Much of a plant's footprint is set minute by minute, by how hard each furnace, kiln and mill is run. Imubit runs those decisions in closed loop, inside the envelope your engineers set, so the same product takes less fuel, makes less waste and emits less.
- 15 to 30%reduction in energy consumption where energy is the optimization target
- 1 to 3%average yield improvement across deployments
- 5 to 10%grinding-energy savings in mining, minerals and metals
- Over 100closed-loop controllers deployed worldwide
Running back from the limit costs fuel and emissions.
Plants keep a cushion between the operating point and the limit, because the unit moves faster than people can follow it. Closed loop watches it every minute, holds it steadier and lets it run closer to its best point. The cushion you no longer need is fuel, power and emissions you no longer spend.
Where the savings come from.
Each is a recurring decision the plant makes every minute. Closed loop makes it the same way, at the best point, every time.
More product from every tonne of feed.
When a unit runs below its best yield, the plant processes more feed to meet the same demand, and each extra tonne brings more low-value streams, more energy and more emissions.
The models learn how the unit actually responds and hold it at its best yield, including through changes in feed composition. Oxbow runs its calcining kilns in closed loop with Imubit: more calcined coke from the same kiln, on less natural gas.
The same product on less fuel.
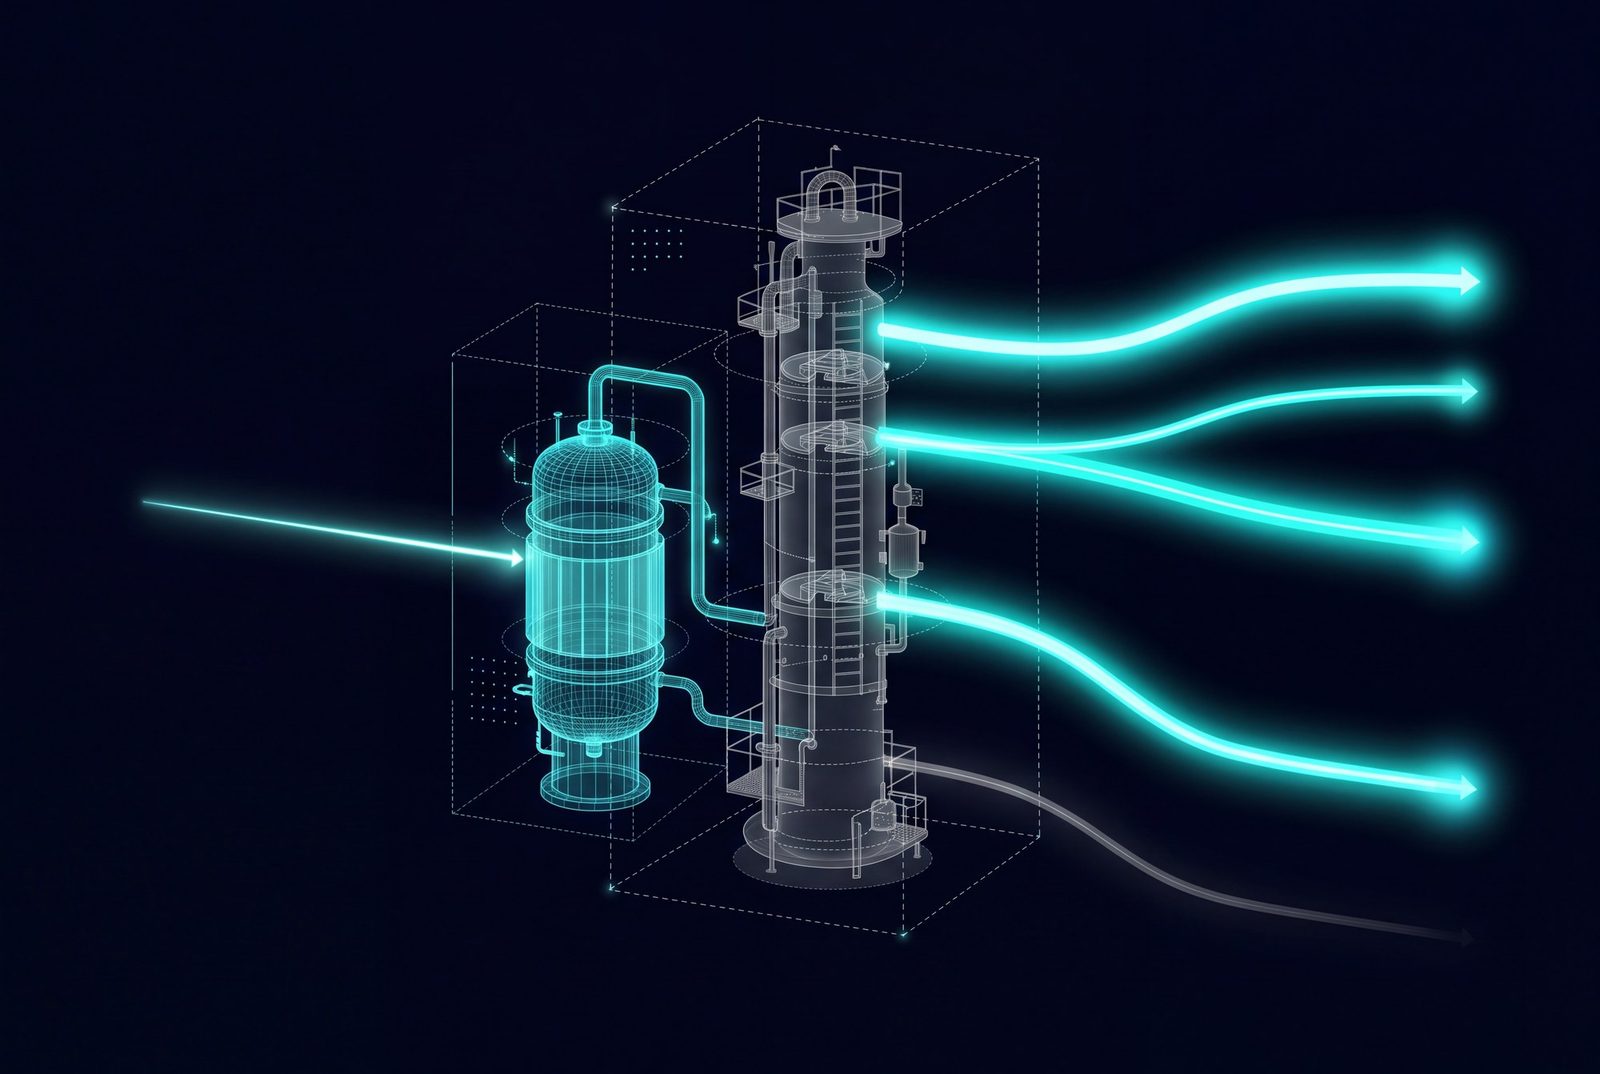
The models can be trained to minimize energy and greenhouse gas emissions while they meet quality targets, and they keep adapting as feed, fouling, catalyst activity and weather change.
Fuel burned on site counts toward Scope 1, so firing less fuel for the same product lowers those emissions directly.
Inside the permit limit through feed changes.
Limits on SOx, NOx and CO protect the people who live near a plant. They are hardest to hold during transients, so plants either risk an excursion or run conservatively and pay for it in efficiency.
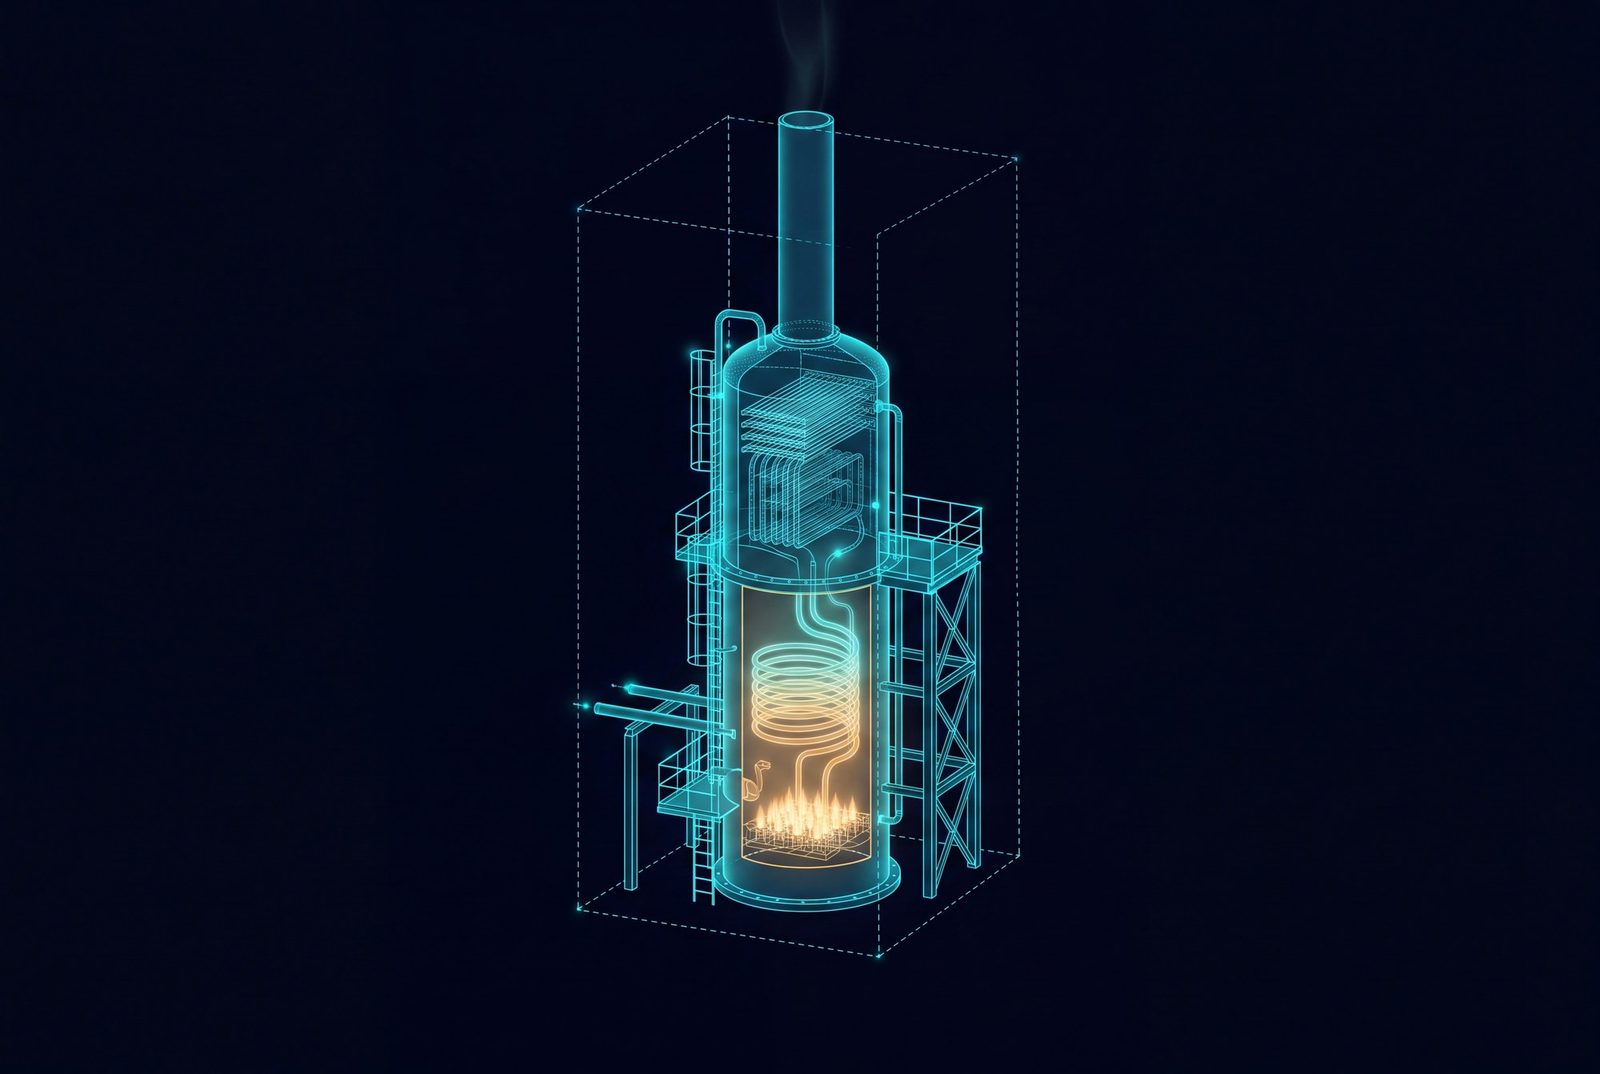
Because the models are dynamic, they predict emissions through the transient and keep the unit inside its limit while it runs efficiently.
Steady product quality as renewable feeds change.
Renewable feeds change in composition from one source to the next, run alongside conventional feeds and react to the weather.
The models account for each change and move the key handles of the unit to keep it efficient, in renewable diesel, co-processing and ethanol.
Renewable diesel optimization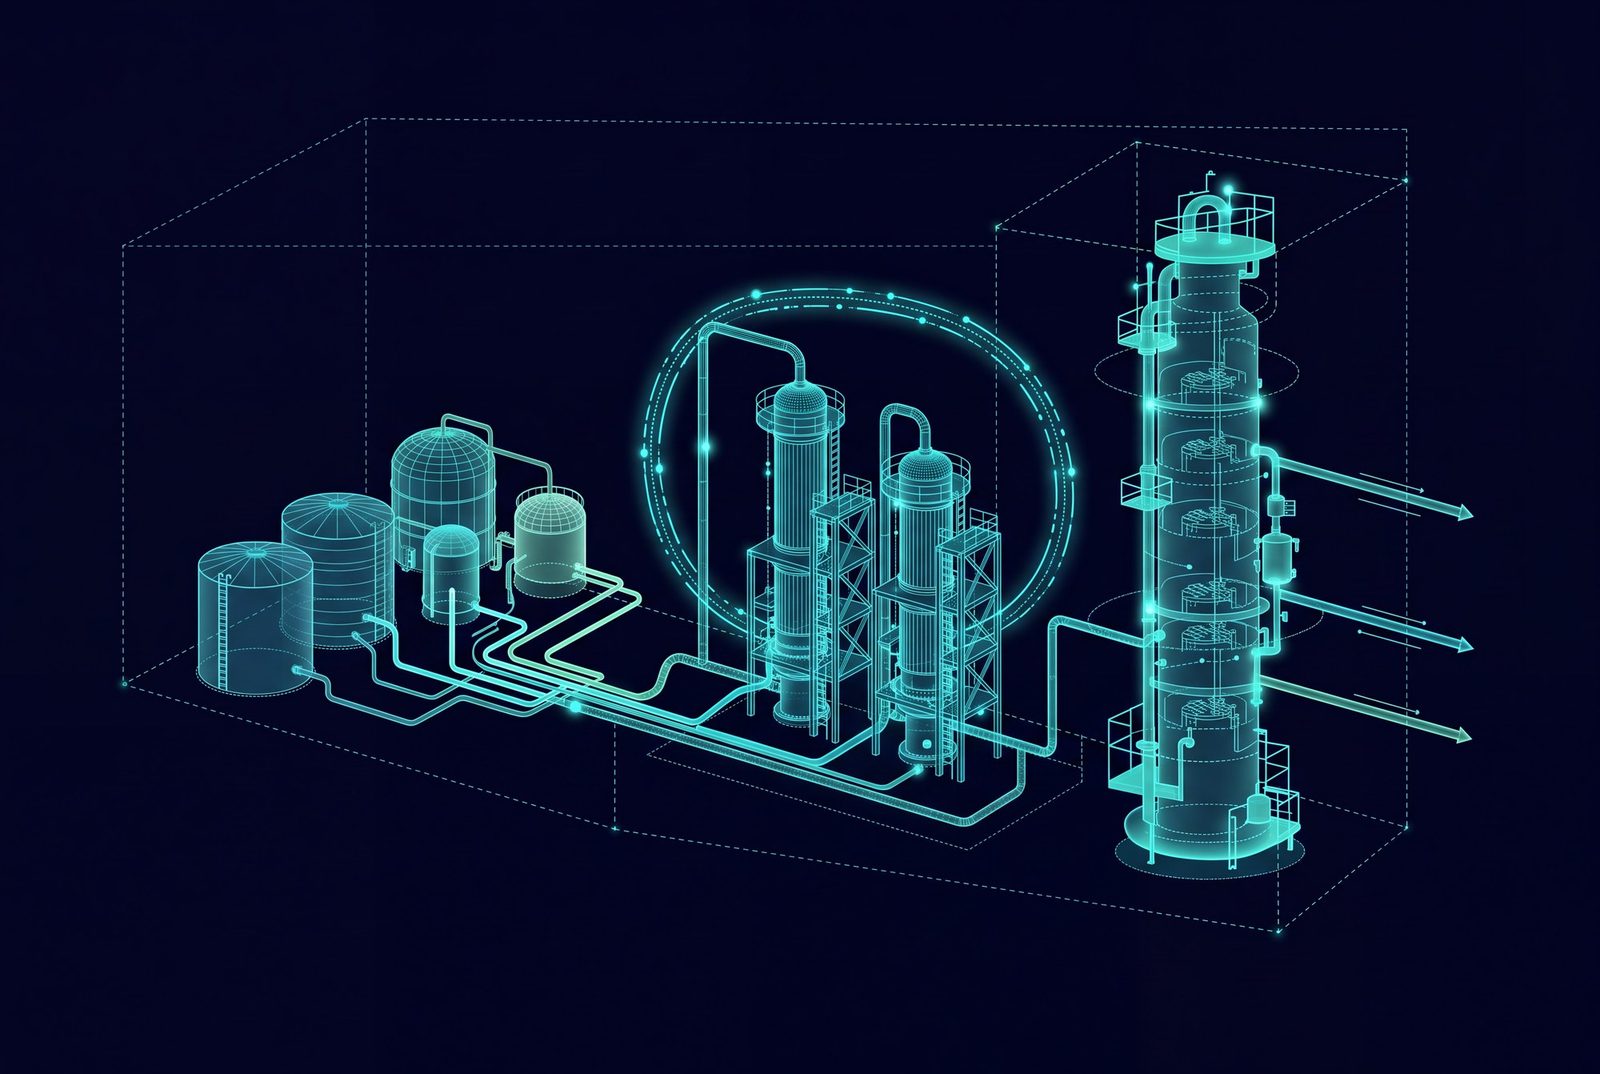
By industry.
Refining
Preem is applying closed loop to the FCC at its Lysekil refinery, to cut emissions and fuel use through the unit's yield profile and a steadier fuel gas balance.
Oil and gasChemicals and polymers
Higher yields and less downtime take less energy per pound of product, and help build carbon reduction into the case for debottlenecking.
Chemicals and polymersCement
A steadier kiln needs less overburning as a safety margin, and consistent clinker quality lowers energy in calcination and grinding.
CementMining and minerals
Holding grind size on target lets the circuit run to the mill's power limit and use less flotation reagent, with 5 to 10% grinding-energy savings.
Mining and minerals
Running in closed loop.
Oxbow, a producer of calcined petroleum coke, runs its rotary kiln operations in closed loop with Imubit. Higher yield means more calcined coke from the same kiln, and the kiln uses less natural gas while it meets product specifications.
Preem, Sweden's largest fuel company, partnered with Imubit in 2025 to apply closed-loop optimization to the FCC at its Lysekil refinery.
Read the Oxbow storyWorking with Imubit allows us to leverage cutting-edge AI to optimize our renewable processes while minimizing our carbon footprint.
Erika Wikström, SVP of Technology, Preem
In depth
Yield and waste
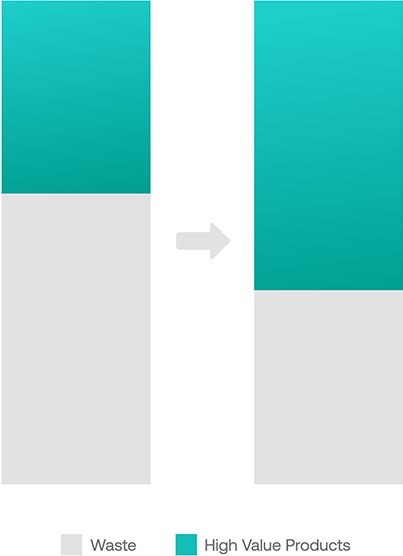
When a unit runs below its best yield, the plant has to process more feed to meet the same product demand. The extra feed brings more low-value and waste streams, more energy per tonne of product, and more greenhouse gas emissions.
The models learn the actual relationships in the unit and control its key parameters continuously. The unit then makes more high-value product and less waste from each tonne of feed, and meets demand at a lower carbon footprint. Across Imubit deployments, that shows up as a 1 to 3% average yield improvement.
The models also pick up small changes in feed composition. That matters most in feed-flexible and co-processing units, where it lets the plant capture more of the economic and environmental value of each unit of throughput.
Oxbow, a producer of calcined petroleum coke, runs its rotary kiln operations in closed loop with Imubit. Higher yield means more calcined coke from the same kiln, and the kiln uses less natural gas while it meets product specifications. Oxbow's SmartKiln® decarbonizes through that yield improvement. Read the Oxbow story.
Energy efficiency
The models can be trained to minimize energy consumption and greenhouse gas emissions while they meet quality standards. They control the critical parameters to find the most efficient operating point for the plant, and they keep adapting as feed composition, fouling, catalyst activity and weather change. Where energy is the optimization target, Imubit deployments have delivered a 15 to 30% reduction in energy consumption. Fuel burned on site counts toward Scope 1 emissions, so firing less fuel for the same product lowers those emissions directly.
The main energy levers differ by industry.
- Chemicals and polymers. Running more efficiently, with less downtime and higher yields, takes less energy per pound of finished product. The models also learn how operating strategies drive energy consumption, which helps build carbon reduction into the case for future debottlenecking projects.
- Cement. A more stable kiln reduces the need to overburn clinker as a safety margin, and consistent clinker quality lowers energy use in calcination and grinding.
- Mining and minerals. Grinding is the most energy-intensive step in mineral processing. Its losses come from variable ore and the lack of a real-time particle size measurement in the mill. Holding particle size distribution on target lets the circuit push to the mill's power-draw limit, raise throughput and use less reagent in flotation. In mining, minerals and metals, Imubit's published results include 5 to 10% grinding-energy savings.
In refining, Preem, Sweden's largest fuel company, partnered with Imubit in 2025 to apply closed-loop optimization to the fluid catalytic cracking (FCC) unit at its Lysekil refinery. The aim is to reduce emissions and fuel use by improving the unit's yield profile and stabilizing the refinery's fuel gas balance.
Working with Imubit allows us to leverage cutting-edge AI to optimize our renewable processes while minimizing our carbon footprint.
Respecting environmental limits
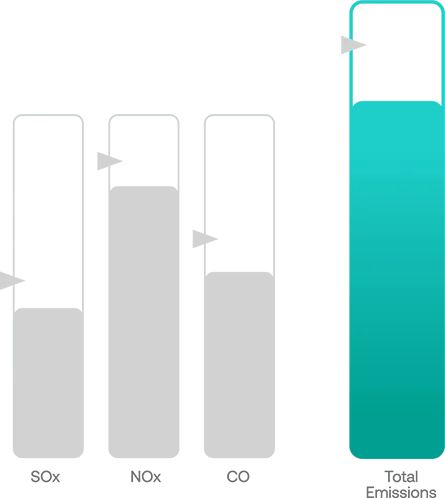
Limits on emissions such as SOx, NOx and CO protect the people who live near a plant. Managing them over time is often a manual task that is not done continuously. Control is hard because the plant is interdependent and its process relationships are nonlinear. Limits are hardest to hold during transients, which are frequent in refineries and petrochemical plants. Plants then either violate environmental constraints or run conservatively to avoid violations, and the conservative margin costs efficiency elsewhere.
The models are trained to respect critical environmental limits in real time while they maximize margin. A limit can be adjusted, or calculated over a longer duration, so the plant runs efficiently while environmental deviations stay small. Because the models are dynamic, they predict key emissions variables more accurately through transients, which lowers environmental impact and makes control safer.
Renewable fuels and ethanol
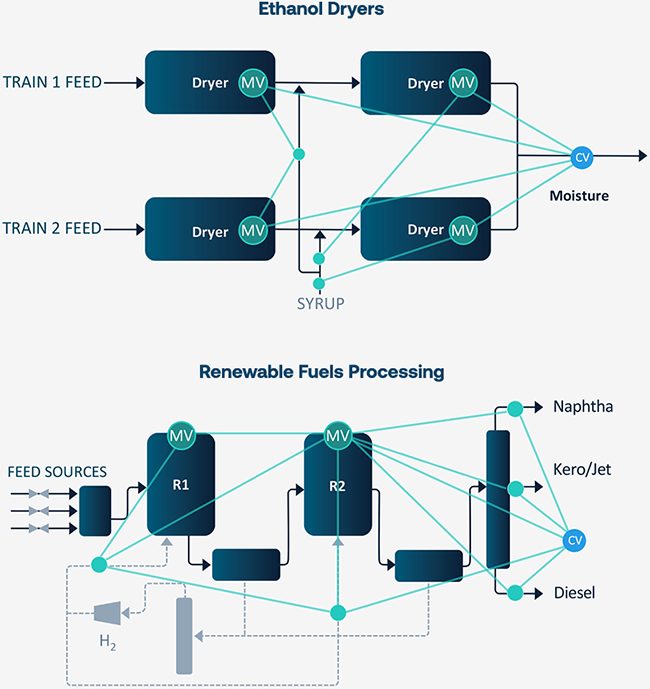
Renewable processes add their own complexity: feeds that change in composition from one source to the next, co-processing with conventional feeds, and sensitivity to ambient conditions. The models account for changes in composition and ambient conditions and adjust the key handles of the plant to keep it efficient and profitable. They apply to continuous renewable processes such as ethanol production and renewable fuels.
The diagram shows two examples. In ethanol drying, two feed trains pass through dryers in series, with syrup added, and the controller moves each dryer's manipulated variables to hold product moisture. In renewable fuels processing, several feed sources pass through two reactors with hydrogen recycle and then a fractionator, and the controller moves the reactor handles to optimize the naphtha, kero and jet, and diesel yields.
For a closer look at one renewable process, read Renewable diesel optimization.
Related reading
Energy strategy first, sustainability as a result
Energy is still one of the largest operating costs in process plants, and four tests help leaders choose energy projects with verifiable results.
AI and carbon emissions, the full picture for industrial operations
AI data centers add emissions, but AI applied to fired heaters, boilers, kilns and conversion units in process plants can cut far more than it adds.
Renewable diesel optimization
How variable feeds, carbon-intensity credits and nonlinear yield trade-offs complicate renewable diesel units, and where closed-loop control fits.
Find out what your gap to plan is costing you.
One to two hours for your team to prepare and upload the data package
Results within a few working days of approval
No workshops
Send your data as it is. Gaps, outages and noisy tags are normal, and our engineers screen and clean them in the platform. If anything limits a use case, we tell you.